
主要特点
编带是没有人算过成本的那道工序
问 THT 产线的节拍,您会得到插件、波峰焊和测试的答案。问手工成型并编带径向元件要多少时间,会议室会安静下来。这通常是唯一一道由「能安排多少人坐在工作台前」决定整条线产量的工序。
到不了测试机的极性错误
把径向电解电容反插,它会通过简单的通断检查。几周后它在客户端失效,外壳开裂。靠肉眼在工作台上分极性,就是把这个失效放进您的保修数据里,而不是废料箱里。
您买的每一卷,都是一条您没有控制的编带
预编带元件很方便,直到插入机开始取料异常——那时的争论就变成您的产线和一家您无法审核的供应商之间的事。自己编带,就把编带规格——间距、孔径、编带高度、极性方向——移进您自己的流程里,您可以改。
规格参数
数据均摘自 Southern Machinery 公开资料。两个来源不一致时,同时列出两个数值及其出处。
| 型号代码 | S-300B Fully Automatic High-Speed Molding and Taping Machine · S-300B Automatic Molding and Taping Machine · S300B radial (LED) lead components taping machine · DT-300BSTD 全自动成型编带机 - supplier model, same machine class |
|---|---|
| 设备功能 | Automatic lead forming (moulding) and taping of radial lead components, with testing and sorting · Fully automatic high-speed moulding and taping of radial components, testing and sorting good from defective · Radial and LED lead forming and taping · Automatic forming and taping of radial lead components |
| 控制系统 | Single-chip microcomputer as the core control unit · The world's most stable brand PLC, or a single-chip control system · Not stated · Single-chip control system |
| 操作界面 | Liquid-crystal display for order placement, simulating the status of each control point · Touch-screen operation interface · Touch screen visible in the walkthrough · Touch screen with alarm display and parameter pages |
| 编带速度 | 180 ± 20 PCS/minute · 180 ± 20 pieces per minute; speaker notes also quote up to 200 pieces per minute · Not stated · 120 - 180 PCS/minute normal operating speed |
| 元件直径 — 标准 | Ф6 - Ф10 mm · Ф6 - Ф10 mm standard fixture configuration · Not stated · Ф3 - Ф10 mm |
| 元件直径 — 夹具套件 | Ф4 - Ф6 share one set of fixtures, Ф8 - Ф10 share another; conventional range Ф4 - Ф10 · Two fixture sets, one for Ф4-Ф6 and one for Ф8-Ф10; other sizes within Ф4-Ф10 to order · Not stated · Not stated |
| 元件长度 | L = 5 - 30 mm · 5 mm to 30 mm · Not stated · 5 - 30 mm |
| 成型引脚间距 — 标准 | 2.5 mm, 3.5 mm, 5.0 mm · 2.5 mm, 3.5 mm, 5.0 mm · 2.5 mm lead shown being formed, 5.0 mm die described · 2.0 mm, 2.5 mm, 3.5 mm, 5.0 mm |
| 成型引脚间距 — 订制 | 7.5 mm, 10 mm, 15 mm and above, ordered separately · 7.5 mm, 10 mm and 15 mm custom pitches can be ordered · Not stated · 7.5 mm and above optional |
| 编带孔距 | 12.7 mm standard; other hole pitches customised on request · 12.7 mm standard · Not stated · 12.7 mm, with 15 mm optional |
| 编带孔径 | 4.1 mm · 4.1 mm · Not stated · Ф4 mm with a tolerance of plus 0.2 mm |
| 编带高度(孔中心至元件底部) | 17 mm - 21 mm · 17 mm - 21 mm · Not stated · 17 - 22 mm |
| 极性选择 | Not stated · Not stated · Positive lead or negative lead first, selectable; the machine re-orients the part to suit · Positive lead first or negative lead first, two selectable modes |
| 包装方式 | Boxed or coiled · Boxed (ammo packing) and coiled (reel) packing methods both supported · Not stated · Boxed as standard, coiled optional |
| 纸带 | Not stated · Not stated · Not stated · 18 mm wide, 0.38 mm or 0.47 mm thick, selected to the product |
| 上带宽度 | Not stated · Not stated · Not stated · 6 mm, 10 mm, 12 mm or 15 mm, selected to the product |
| 引脚剪裁 | Not stated · Not stated · Leads beyond roughly 25 mm are trimmed at the cutting station before taping · A cutting station removes the excess where the lead is too long |
| 不良品处理 | Good and defective products sorted automatically when the tester is fitted · Defective products sorted out automatically · The eject gate opens for a good part and drops a failed part into a scrap tube · The eject gate closes for a good part and opens to reject a defective part |
| 驱动系统 | Servo control system replacing the traditional clutch · Servo control system replacing the traditional clutch · Not stated · Servo control system replacing the traditional clutch |
| 凸轮精度 | All cams imported, grinding accuracy 0.01 mm · Imported cams ground to 0.01 mm accuracy · Not stated · All cams imported, grinding accuracy 0.01 mm |
| 机架 | Square rack feeder, precision fixtures of special materials on an accurate centre line · Not stated · Aluminium profile frame with branded panels visible in the walkthrough · Imported aluminium profile frame, corrosion resistant |
| 电源 | 220 V / 50 Hz / 1.6 kW · 220 V / 50 Hz / 1.6 kW · Not stated · 1 HP motor, 220/380 V, 50/60 Hz |
| 气压 | 4 - 5 kg/cm² · 4 - 5 kg/cm² · Not stated · 4 - 5 kg/cm² |
| 外形尺寸(长 × 宽 × 高) | 2200 × 1200 × 1500 mm · 2200 × 1200 × 1500 mm · Not stated · Not stated |
| 设备重量 | 700 - 900 kg · 700 - 900 kg · Not stated · Not stated |
型号、对比与待确认事项
Where the documents disagree (6 行)
| Parameter | What the S-300B documents say | What the other source says | What the difference means | Status |
|---|---|---|---|---|
| Model naming | The product sheet and the presentation deck both call the machine S-300B. The walkthrough video calls it S300B, without the hyphen. | The image library also holds a machine photographed and labelled S-300BSTD, and the supplier manual supplied with the enquiry covers a DT-300BSTD. | Four codes circulate for what is presented as one machine class. S-300B is the code the product sheet and the deck agree on, so it is the code used on this page. If your quotation names S-300BSTD, ask which of the two it is - they are not the same build. | To be confirmed |
| Control system and operator interface | The product sheet describes a single-chip microcomputer as the core control unit, with a liquid-crystal display for order placement that simulates the status of each control point. | The presentation deck describes the world's most stable brand PLC or a single-chip control system, with a touch-screen operation interface. | One document describes a fixed LCD annunciator panel and the other a touch screen, and they do not describe the same hardware. The machine photographs show a colour touch panel. This matters at quotation time: a touch panel and an LCD annunciator are different spares, different training and different prices. | To be confirmed |
| Taping speed | The product sheet states a production capacity of 180 ± 20 PCS/minute, which is a band from 160 to 200. | The presentation deck repeats 180 ± 20 pieces per minute, and its speaker notes then say the machine processes up to 200 components per minute - the top of the band presented as the rate. The supplier manual for this class states 120 - 180 PCS/minute. | Three different framings of the same machine. The band is what the product sheet publishes and what this page quotes. Plan capacity from the bottom of the band, not the top, and treat 200 as a best case rather than a rate. | To be confirmed |
| Component diameter range | The product sheet gives the processed product diameter as Ф6 - Ф10 mm, and separately states that the machine handles a conventional range of Ф4 - Ф10 in which Ф4 - Ф6 share one set of fixtures. | The presentation deck says the standard fixture configuration covers Ф6 - Ф10 mm, with other sizes within the Ф4 - Ф10 range available as custom options. The supplier manual for this class states Ф3 - Ф10 mm. | The product sheet describes Ф4 - Ф6 as part of the conventional range with its own fixture set, while the deck describes that band as a custom option. If you run components below Ф6, confirm whether the Ф4 - Ф6 fixture set is a standard line item or an order - the answer changes both the lead time and the price. | To be confirmed |
| Taping height | The product sheet gives a taping height of 17 mm - 21 mm. | The presentation deck repeats 17 mm - 21 mm. The supplier manual for this class states 17 - 22 mm. | A 1 mm difference at the top of the range. Taping height is set against your inserter's pick height, so if your tape specification sits at 22 mm, ask for it in writing before the order rather than adjusting on site. | To be confirmed |
| Packaging and formed lead pitch | The product sheet lists boxed and coiled packaging as equal alternatives, and gives the standard formed lead pitch as 2.5 mm, 3.5 mm and 5.0 mm, with 7.5 mm, 10 mm and 15 mm and above ordered separately. | The presentation deck lists boxed (ammo packing) and coiled (reel) as both supported. The supplier manual for this class states boxed as standard with coiled optional, and prints an additional 2.0 mm pitch in the standard set. | Two questions to settle in the quotation rather than in the factory: whether coiled output is included or an option on the configuration you are buying, and whether 2.0 mm is a standard die or a special. Neither document is wrong; they describe different configurations. | To be confirmed |
What 180 components a minute is worth over a shift (3 行)
| Taping speed | Components per hour | Components per 8-hour shift | Components per month, 26 days |
|---|---|---|---|
| 160 PCS/min (bottom of band) | 9,600 | 76,800 | 1,996,800 |
| 180 PCS/min (nominal) | 10,800 | 86,400 | 2,246,400 |
| 200 PCS/min (top of band) | 12,000 | 96,000 | 2,496,000 |
详细介绍
从散装料盒到密封编带之间的九个工位
以下工位顺序取自现场走机视频与本机类别的供应商手册。它描述元件行进的顺序,不是机柜的物理布局。
- 散装供料. 振动盘把散装元件从料盒中提升并定向到直线轨道上。盘内的光电开关在轨道满料时停盘,轨道上的光电开关在料少时降低机速——设备跟随供料,而不是和供料较劲。
- 引脚分张. 分张器在其他部件接触元件本体之前先把两根引脚分开。先做这一步,才不会让模具压在交叉的引脚上,也是本机能直接吃袋装料、无需预分选的原因。
- 引脚成型. 一体式成型模具把引脚压到设定间距:标准为 2.5 mm、3.5 mm 或 5.0 mm。模具是整体件,所以换间距就是换模具,而模具四颗螺钉即可拆下。
- 极性检测. 测量元件的极性。对径向电解电容、LED 或二极管而言,这就是「能用的板」和「退回来的板」之间的差别,而且检测发生在元件被编入带之前。
- 方向校正. 若极性与正在编的带相反,方向校正工位会把元件转过来,而不是判它不合格。两个方向都可选,因此编带可以做成正极引脚在前或负极引脚在前,以匹配插入机的期望。
- 数值测试. 装上匹配的测试仪后,设备读取电容值与电阻值并与您设定的窗口比较。这道工位拦下混料——否则错值元件会被编带、装盒、当作良品出货。
- 引脚剪裁. 过长的引脚在编带前剪到长度。标准引脚范围内的元件原样通过;长引脚元件在本工位修剪,使成品编带高度一致,而不是随来料引脚长度变化。
- 不良品剔除. 良品时闸门保持打开,不良品落入滑道。不良品经管路进入废料盒,与良品流物理隔离,因此夜班疲惫的操作员无法把不良品重新放回产线。
钱花在机器内部的什么地方
三件事决定一台编带机第十年还在不在跑:什么驱动它、运动件用什么材料、夹具还能不能买到。这三点都写在产品规格书上,也都能在机器照片里看到。
- 伺服控制取代离合器. 驱动采用伺服控制系统,取代传统机械离合器。在这类设备上,离合器正是会磨损、打滑、最终卡死的部件,也是非计划停机最大的单一来源。去掉它,去掉的是失效模式,不只是症状。
- 进口凸轮,磨削精度 0.01 mm. 所有凸轮均为进口原件,磨削精度 0.01 mm。在每分钟 180 只的速度下,凸轮组决定设备是安静运转还是把自己震散:0.01 mm 就是「稳定的引脚成型」与「每千只早闭一线的模具」之间的差别。
- 特殊材料夹具与一体式模具. 方架供料器、精密夹具与成型模具均采用特殊材料,并在精确的中心线上加工。模具是一体式而非拼装式,因此成型尺寸稳定,换型快且不伤产品。两套夹具覆盖 Ф4-Ф6 与 Ф8-Ф10。
文件之间不一致的地方
一张悄悄从两个数字里挑一个的规格表,价值不如一张把两个都摆出来的表。以下六项参数在所附文件中并不一致,或只出现在其中一份。下单前请逐项对照您配置的现行图纸确认。
每分钟 180 只,一个班下来是多少
公布的区间是每分钟 180 ± 20 只。下表把该区间换算成每小时、每班、每月的数量,让您用来规划的数是您自己选的,而不是别人给您的。
需要配置什么,而不只是列出了什么
编带机只有在模具、夹具和编带都对应您实际要跑的元件时才有用。以下是应当随订单一起定下来、而不是订单之后再说的项目。
- 对应您间距的成型模具. 2.5 mm、3.5 mm、5.0 mm 模具为标准。7.5 mm、10 mm、15 mm 及以上另行订购。换模具是四颗螺钉的操作,因此跑两种间距的工厂可以两套都留。
- 另一档直径范围的第二套夹具. Ф4-Ф6 与 Ф8-Ф10 各用一套专属夹具。如果您的元件混线跨越两档,请随设备一起订两套,而不是在第一次换型时才发现缺口。
- 卷装输出取代盒装. 盒装(弹匣式 ammo 包装)是标准输出。若您的插入机使用卷盘,则需要指定卷装配置——请参见「待确认项」表,因为两份所附文件对此说法不一。
- 电容与电阻测试仪. 装上匹配的测试仪后,测试与分选功能才生效。没有它,设备照样成型编带;有了它,设备还能在元件进入编带之前剔除超出窗口的件。
- 非标准编带孔距. 12.7 mm 为标准。其他孔距可订制,本类别供应商文档中 15 mm 作为选配出现——请对照您插入机的编带规格确认。
- 对应您元件的振动盘与轨道治具. 振动盘与直线轨道按元件本体加工。请提供图纸与实物样品,因为能跑 6 mm 电解电容的盘,不一定能跑同直径的方形 MKT。
从您的元件清单到一条已验证编带的六个步骤
做事的顺序比速度更重要。多数被归咎于设备的编带机问题,其实是在模具开切之前从未谈定的编带规格。
- 确认编带规格. 在动手做任何东西之前:引脚间距、极性方向、编带高度、孔距、纸带宽度与厚度、上带宽度、盒装或卷装。这一份文件决定了模具、夹具与耗材。
- 确认元件. 提供元件图纸与实物样品。本体直径、本体高度、引脚直径、引脚长度与本体形状都会改变夹具与振动盘治具。
- 准备场地、电源与气源. 220 V 单相 1.6 kW,4-5 kg/cm² 的洁净干燥空气,以及能承受 700-900 kg 设备的水平地面。四侧都要留出通道:振动盘、废料管与出料端都必须够得到。
- 调整振动盘与轨道. 盘振幅、轨道光电位置与分张器都是对照实物元件调的,不是对照图纸。这一步做不好,三周后会以速度问题的形式出现。
- 验证第一条编带. 跑完整一卷,然后测量:间距、编带高度、极性方向、孔位,并把样品对照元件图纸核验。把这条量过的带留作该设备整个寿命期的基准。
- 交付并附保养卡. 对触摸屏、参数页面与报警清单做操作培训,并附一张书面保养卡,写明润滑点与凸轮、光电的检查周期,供您自己归档。
设备到厂之后会发生什么
编带机既是设备采购,也是治具项目。以下是决定它能否持续运转的四个服务环节。
视频
来自 Southern Machinery YouTube 频道的视频。点击播放前不会从 YouTube 加载任何内容。
产品目录与资料
- PDFS-300B Fully Automatic High-Speed Molding and Taping MachineS-300B product sheet
- PDFSM-301 Taped Radial Capacitor Lead Cutter en-USRadial taping process manuals
- PDFS-C45 Auto Taped radial lead cutting machine User ManualRelated forming and taping product sheets
- PDFTaped components lead cutting forming machineRadial taped feeder drawings
- PDFSJL80A SMD REEL TAPING MACHINERadial taped feeder drawings
- PDFTHT radial taped feeder 3DRadial taped feeder drawings
- PDFSMT Radial LED taped feeder UIC 3DRadial taped feeder drawings
- 3DThe full Southern Machinery video board
- 3DThe full Southern Machinery product catalogue board
- LINKMachine catalogue - file.autoinsertion.com
工程笔记
ARTICLE 01Your THT line is not slow at insertion, it is slow at the bench before it
The station that sets your line rate is usually the one nobody has a cycle time for. Body text is kept in English on every language version by design: these are technical articles, and a machine-translated technical article is worse than an English one. Ask a production manager for the cycle time of a THT line and…
ARTICLE 02The polarity mistake that reaches the customer, not the tester
Why a reversed electrolytic capacitor passes every simple check you run in-house. Body text is kept in English on every language version by design: these are technical articles, and a machine-translated technical article is worse than an English one. Here is a failure that passes your end-of-line test, passes your…
ARTICLE 03How to size a radial taping machine from a component list
Diameter, body height, lead diameter and lead length decide the machine, not the model number. Body text is kept in English on every language version by design: these are technical articles, and a machine-translated technical article is worse than an English one. The most expensive mistake in buying a taping machine…
ARTICLE 04Boxed or reeled: the tape specification your inserter actually wants
Six numbers on a tape drawing that decide whether the inserter picks or mis-picks. Body text is kept in English on every language version by design: these are technical articles, and a machine-translated technical article is worse than an English one. A tape is a mechanical interface, and like every mechanical…
ARTICLE 05What 0.01 mm of cam accuracy is buying you at 180 parts a minute
The arithmetic that turns a grinding tolerance into a defect rate. Body text is kept in English on every language version by design: these are technical articles, and a machine-translated technical article is worse than an English one. 0.01 mm sounds like a marketing number until you multiply it by 180 a minute. Then…
ARTICLE 06Running a taping machine for fifteen years: what actually decides it
Three assemblies fail before the frame does, and all three are replaceable by design. Body text is kept in English on every language version by design: these are technical articles, and a machine-translated technical article is worse than an English one. A taping machine does not die of old age. It dies of three…
常见问题
S-300B 能给哪些元件编带?
径向引脚元件:电解电容、MKT 与金属化电容、LED、三极管、钮子开关、电感、晶振、PTC 热敏电阻、连接器、橡胶套以及其他针脚类零件。标准夹具配置覆盖本体直径 Ф6 至 Ф10 mm、长度 5 至 30 mm;产品规格书另述用两套夹具覆盖 Ф4 至 Ф10 mm 的常规范围。若您的元件在此之外,请提供图纸,因为振动盘与夹具都是按本体加工的。
它会检测元件,还是只做编带?
装上匹配的测试仪,两者都做。设备检测每一只元件的极性;装上测试仪后,还会读取电容值与电阻值并与您设定的窗口比较。超出窗口的元件被剔入废料管而不是编带。没有测试仪,设备照样成型编带,只是不再按数值剔除。
盒装与卷装能同时做吗?
产品规格书把盒装与卷装列为对等选项,演示文稿称两者都支持。本类别的供应商手册写标准为盒装、卷装为选配。由于两份文件不一致,本页把它列为待确认项:告诉我们您的插入机用哪种输出,我们在报价时确认,而不是让您到现场才发现。
它用什么编带和纸带?
纸带宽 18 mm,厚 0.38 mm 或 0.47 mm;上带按产品选用 6、10、12 或 15 mm;链轮孔距 12.7 mm,孔径 4.1 mm。这些耗材数字来自本类别设备的供应商手册,它是所附文件中唯一印出这些数据的文件——因此在大批订购耗材之前,请对照您的编带规格确认。
它到底有多快?
公布的区间是每分钟 180 ± 20 只,即 160 至 200。请按区间下限规划,把 200 当作最佳情况。本页的产能表把该区间换算成每小时、每班、每月的元件数,并假设设备整段时间都在运转——用来规划之前请先乘以您自己的可用率。
换一次引脚间距要多久?
成型模具是一体式,四颗螺钉即可拆下,产品规格书把快速拆装列为设计特点。因此换间距就是换模具,不是重新调机。更花时间的是首件验证——在放行量产之前,先对照您的编带规格测量第一条编带。
设备在现场需要什么条件?
220 V 单相 1.6 kW,4 至 5 kg/cm² 的洁净干燥空气,以及能承受 700 至 900 kg 设备、占地 2200 × 1200 × 1500 mm 的水平地面。四侧留出通道:散装振动盘、废料管与出料端在一个班内都必须够得到。
怎么获取报价?
请提供元件图纸或料号、您插入机使用的编带规格,以及您的月用量。有这三样,我们就能在报价单上写明模具、夹具套件、振动盘治具与输出配置,而不是罗列选项让您去猜。如果还没有编带规格,也请直说——我们把空白表发给您。
相关产品
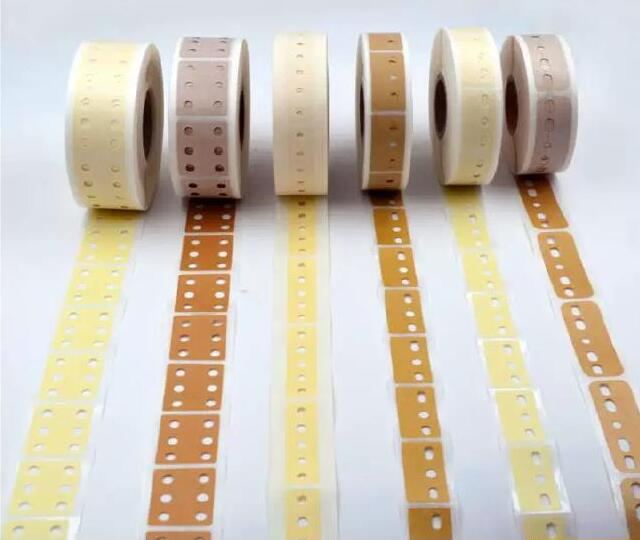
AI 立式插件机接料带 三孔/五孔/六孔 与接料剪
适用于径向(立式)自动插件机的 AI 接料带:三孔、五孔(六孔可定制),美纹纸或牛皮纸,高粘性,正反面精密模切,另配 12.7 / 15.0 mm 径向编带接料剪。

SMT 飞达校准治具 - 面向智能 EMS 工厂 PCB 组装的飞达精度可视化检查台
飞达回到产线前,先检查取料位置、供料动作与对位状态。CCD 相机、LCD 显示器、X/Y/H 三轴微调、FUJI NXT 飞达基座。220V、45kg,每个数值均标注来源。
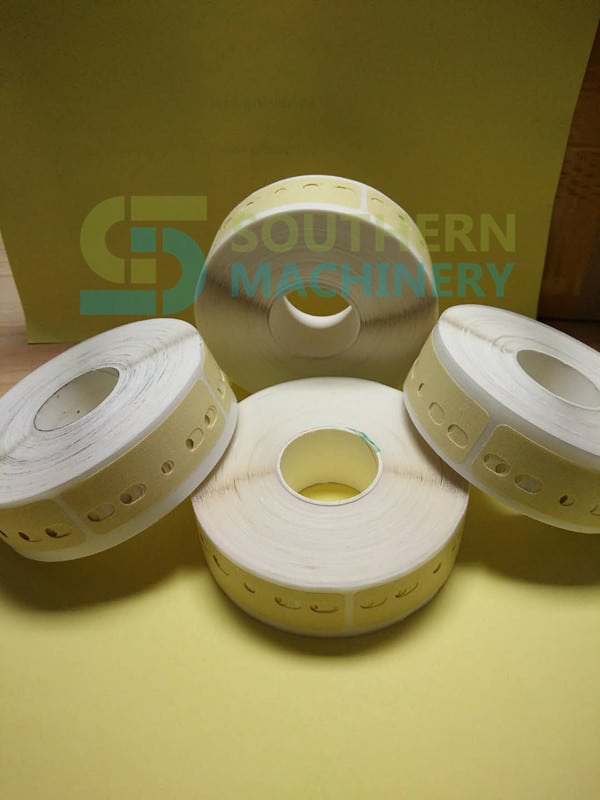
THT 径向元件接料带(3/5/6孔)自动插件机专用
高粘 AI 接料带,适用于 THT 径向编带元件(电容、电感、二极管)12.7 mm 与 15.0 mm 带材。美纹纸/牛皮纸基材,精密模切 3/5/6 孔,不留残胶,接料不停机,效率提升 15%。南方机械 SCT 系列。
本页部分技术内容(表格、资料标题)按原文以英文显示。
索取报价:S-300B 径向元件成型编带机 - 南方机械
发送您的电路板、元件清单或机型,我们将回复配置方案与报价。价格按项目核定。