
Axialbestückautomat S4000 für die smarte EMS-THT-Leiterplattenbestückung
Axialbestücker S4000: veröffentlichte Höchstgeschwindigkeit 20.000 CPH, 5–60 modulare Feederstationen, Bestückung in jedem Winkel auf einem Servo-Drehtisch, doppelte Drahtbrücken-Feeder, Platinendicke 0,79–2,36 mm, Platinen 50 x 50 bis 400 x 300 mm. Servoangetrieben, EtherCAT, MES-fähig.
Der S4000 bestückt gegurtete Axialbauteile – Dioden, Widerstände und Drahtbrücken – in jedem Winkel in Durchgangslöcher, schneidet und formt die Anschlüsse und biegt sie in einem durchgehenden Zyklus um. Eine modulare Feederbank von 5 bis 60 Stationen, doppelte Drahtbrücken-Feeder, Lochkorrektur per Bildverarbeitung und ein MES-fähiger Datenpfad.
Wichtigste Merkmale
Ein Zyklus statt vier Handgriffe
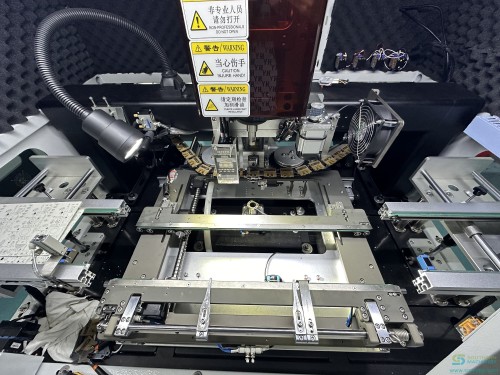
Ein Bediener greift das Teil, prüft die Polarität, biegt die Anschlüsse auf das Lochraster, steckt es ein und dreht dann die Platine zum Umbiegen um. Der S4000 erledigt all das in einem Bestückzyklus: Der Kopf schneidet die Anschlüsse von der Kette, formt sie, drückt sie durch die Löcher, und der Abschneider unter der Platine biegt sie um. Der Bestückkopf trägt drei symmetrische Werkzeugpaare – oberer Schneider,…
Jeder Winkel, nicht nur 0 und 90 Grad
Die Platine liegt auf einem servoangetriebenen Drehtisch. Die R-Achse dreht die Platine für jede Zeile des Bestückprogramms auf den programmierten Winkel, sodass ein Layout mit einer 30-Grad-Diode oder einer diagonalen Drahtbrücke dieses Teil nicht mehr an den Handarbeitsplatz zurückzwingt. Das Handbuch beschreibt es als Bestückung in jedem Winkel in festgelegter Reihenfolge, mit dem Drehwinkel pro Programmzeile gespeichert.
Drahtbrücken ohne Gurtschritt
Drahtbrücken aus der Trommel werden in Z- und Y-Richtung gerichtet und von einem eigenen W-Achsen-Motor zum unteren Schneider geführt, dann von der Bestückwelle eingesetzt. Die Broschüre von 2024 gibt an, dass die Maschine Drahtbrücken direkt ohne Gurt bestückt und dass eine Doppelfeeder-Anordnung zwei Drahtspezifikationen – 0,5 mm und 0,6 mm – gleichzeitig verarbeitet. Southern Machinery dokumentiert dies…
Spezifikationen
Werte wie in den Unterlagen von Southern Machinery veröffentlicht. Widersprechen sich zwei Quellen, werden beide Werte mit Quelle gezeigt.
| Model | S4000 Axial Inserter · S4000 Axial Insertion machine 2024 (product brochure) |
|---|---|
| Top speed | 20,000 CPH · Brochure and series manual (manual states 20,000 points per hour) |
| Actual speed | 10,000 CPH · S4000 Axial Insertion machine 2024 (product brochure) |
| Component types | Axial tape-and-reel packages: diodes, resistors, jumper wire. Barrel-fed jumper wire fed independently. · Brochure and series manual (manual states 20,000 points per hour) |
| Lead diameter | 0.3 – 0.8 mm · Brochure and series manual (manual states 20,000 points per hour) |
| Insertion angle | Any angle, adjustable, on the servo rotary table · S4000 Series Manual V1.1, section 1.3 item 5 |
| Lead cutting length | 1.2 – 2.2 mm (adjustable) · S4000 Series Manual V1.1, section 1.3 item 5 |
| Lead bending angle | 0 – 35° (adjustable) · S4000 Series Manual V1.1, section 1.3 item 5 |
| Component height allowed | 15 mm standard, customisable on request · S4000 Series Manual V1.1, section 1.3 item 5 |
| Available PCB size | 50 x 50 mm to 400 x 300 mm (brochure) / maximum 330 x 300 mm (manual) · Conflicting — both values shown in the disclosure table below |
| PCB thickness | 0.79 – 2.36 mm · Brochure and series manual (manual states 20,000 points per hour) |
| Component lead span | 5.00 – 20.00 mm (brochure) / 5.0 – 22 mm (manual) · Conflicting — both values shown in the disclosure table below |
| Feeder stations | 5 / 10 / 20 / 30 / 40 / 50 / 60 available (brochure) / 10 / 20 / 30 / 40 configurable (manual) · Conflicting — both values shown in the disclosure table below |
| Hole position correction | Machine vision automatic alignment, multi-point MARK correction · S4000 Series Manual V1.1, section 1.3 item 5 |
| PCB conveying | In-line automatic loading and unloading, left to right or right to left, with a custom manual version available · S4000 Series Manual V1.1, section 1.3 item 5 |
| Drive system | Custom absolute servo drive, eliminating dozens of photoelectric sensors · S4000 Series Manual V1.1, section 1.3 item 5 |
| Control system | Bus-based multi-axis control, EtherCAT motion control card, industrial PC with router · Series manual section 1.3 item 16 and brochure page 3 |
| Operating system | Chinese / English interface on a Windows 7 control platform (manual) — brochure lists Windows-based operation · Series manual section 1.3 item 16 and brochure page 3 |
| Data input | USB input in Excel file format; online and offline program editing both supported · S4000 Series Manual V1.1, section 1.3 item 5 |
| Smart factory | 4G IoT, MES-compatible, black-box data logging · S4000 Series Manual V1.1, section 1.3 item 5 |
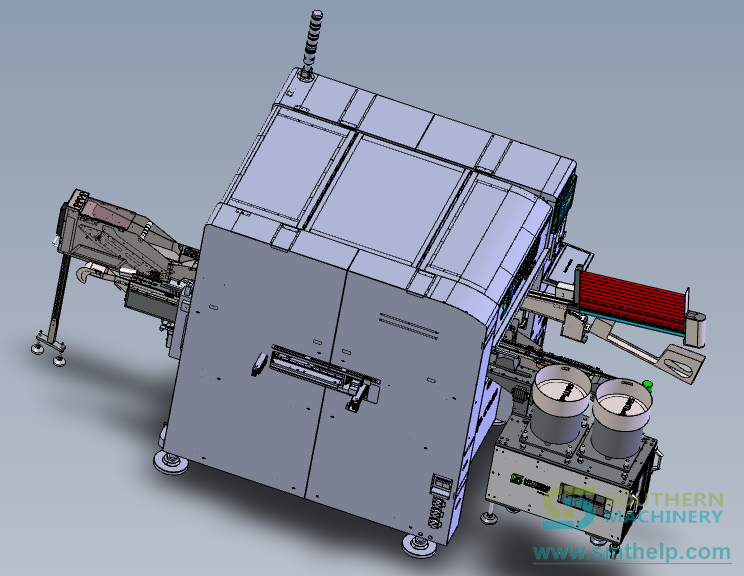
| Machine dimensions | Main machine 1780 x 1500 x 1600 mm; auxiliary machine 500 x 900 x 1000 mm; 10-station material station 850 x 900 x 1360 mm; 20-station material station 1400 x 900 x 1360 mm · S4000 Series Manual V1.1, section 1.3 item 5 |
| Weight | 850 kg standard version (manual) / 880 kg (brochure) · Conflicting — both values shown in the disclosure table below |
| Power supply | Single-phase AC 220 V, 50/60 Hz, 1.6 kW (L+N+E) · Brochure and series manual (manual states 20,000 points per hour) |
| System protection | Multiple protections including an isolation transformer · S4000 Series Manual V1.1, section 1.3 item 5 |
| Air source | 0.6 – 0.8 MPa (brochure) / 0.5 – 0.7 MPa (manual) · Conflicting — both values shown in the disclosure table below |
| Air consumption | 0.3 m³/min · S4000 Series Manual V1.1, section 1.3 item 5 |
| Operating ambient temperature | 5 – 28°C · S4000 Series Manual V1.1, section 1.3 item 5 |
| Machine noise | 65 – 75 dB · S4000 Series Manual V1.1, section 1.3 item 5 |
| Insertion defect rate | < 500 PPM · S4000 Series Manual V1.1, section 1.3 item 5 |
Modelle, Vergleiche und offene Punkte
The seven axes, in the machine's own names (8 Zeilen)
| Axis | Function as described in the manual | Drive |
|---|---|---|
| X | Moves the worktable left and right; ball screw with two linear guide rails, coupling between screw and motor. | Servo, absolute |
| Y | Moves the worktable front to back on a ball screw; the R worktable is carried on the Y table. | Servo, absolute |
| R | Rotary table. Turns the PCB to the programmed insertion angle; circular guide rail and rotary disk driven by the R-axis reducer through a timing belt. | Servo, absolute |
| H | Insertion axis. Raises and lowers the three tool pairs in the cassette; gear shaft meshed with a rack. | Servo, absolute |
| U | Width or span axis. One motor drives two opposed lead screws so the left and right tool sets open and close together to match the hole pitch. | Servo, absolute |
| B | Base vertical axis. Drives the lead cutters up and down through a gear and rack; shares its drive system with the U axis for synchronised span changes. | Servo, absolute |
| C | Chain axis. Drives the insertion chains and the discharge chain from the main shaft, with a zero-position detection disk at the end of the shaft. | Servo via gearbox |
| W | Jumper axis. Straightens the jumper wire and drives a gear pair to deliver a set length to the lower cutter. | Servo, absolute |
Where the documents disagree, both values stay on the page (7 Zeilen)
| Item | 2024 product brochure | S4000 series manual V1.1 | What it changes for you |
|---|---|---|---|
| Machine dimensions | 1700 x 1500 x 1600 mm | Main 1780 x 1500 x 1600 mm + auxiliary 500 x 900 x 1000 mm | Bay width and floor layout. The 80 mm difference plus the auxiliary frame decides whether the line fits. |
| Weight | 880 kg | 850 kg standard version | Floor loading and the lifting plan for installation. 30 kg is inside normal configuration variance. |
| Available PCB size | 400 x 300 mm | 330 x 300 mm, customisable on request | Whether your largest panel runs as standard or as a custom build. Ask before you commit the panel design. |
| Component lead span | 5.00 – 20.00 mm | 5.0 – 22 mm | Whether your widest axial part is inside the standard range. Parts above 20 mm may need confirmation. |
| Feeder stations | 5, 10, 20, 30, 40, 50, 60 stations available | 10 / 20 / 30 / 40 stations, configurable as needed | How many part numbers you can run without a reel change. 50 and 60 station frames are listed in the brochure only. |
| Air source | 0.6 – 0.8 MPa | 0.5 – 0.7 MPa | What your house compressor has to deliver. Specify the higher figure if you want margin. |
| Speed statement | 20,000 CPH top and 10,000 CPH actual, both printed | 20,000 points per hour, listed as maximum | Your capacity plan. The brochure is the only document that gives a separate actual figure, and it is half the top figure. |
The throughput levers, ranked by how much they usually move the answer (6 Zeilen)
| Lever | Effect on realised rate | How it is controlled |
|---|---|---|
| Number of parts per board | Dominant. A board with 60 axial parts takes six times the insertion time of a board with 10, before any other factor. | Program design; where a part can move to SMT or to a radial machine, the axial count drops. |
| Span changes within the program | High. The U axis has to open or close the tool sets to the new hole pitch, and the lead cutters follow. | Group parts by span when the layout allows it. The program list records the span per line, so this is visible before the board runs. |
| Rotation angle changes | Moderate. The R axis re-orients the table for each programmed angle. | Sequence the program by angle where the board allows, so the table turns fewer times. |
| Feeder station count | Indirect but large. Too few stations means reel changes mid-run, and every change is a stop. | Size the feeder bank against the part count of the whole product family, not the current job. |
| Board transfer and clamping | Fixed per board. The stopper, clamp and conveyor cycle repeat regardless of part count. | Amortised by running larger panels; panelisation in the software builds the multi-board program quickly. |
| Component feed reliability | Multiplicative when it goes wrong. A jam stops the machine rather than slowing it. | Feed mechanism alignment: the three centrelines between distribution head, discharge chain and chain-track guard plates must be coincident, and the chain tension set to 3–5 degrees of slack. |
Im Detail
Axial parts are the last hand-loaded operation on most THT boards
SMT took the chips. Radial inserters took the capacitors. What is left on the bench is usually the axial band — resistors, diodes and the jumper wires that tie a board together. Those parts are cheap, they arrive on tape, and they are still being placed by hand because the volume never looked high enough to justify a machine. That calculation changes when you cost it per board instead of per part.
- One cycle instead of four hand movements. A hand operator picks the part, checks the polarity, bends the leads to the hole pitch, inserts it, then turns the board over to clinch. The S4000 does all of that inside one insertion cycle: the head cuts the leads off the chain, forms them, pushes them through the holes, and the lead cutter beneath the board clinches them. The insertion head carries three symmetric tool pairs — upper cutter,…
- Any angle, not just 0 and 90 degrees. The PCB sits on a servo-driven rotary table. The R axis turns the board to the programmed angle for each line of the insertion program, so a layout that needs a 30-degree diode or a diagonal jumper no longer forces that part back onto the bench. The manual describes it as insertion at any angle in a prearranged sequence, with the rotation angle stored per program line.
- Jumper wire without a taping step. Barrel-fed jumper wire is straightened in the Z and Y directions and delivered to the lower cutter by a dedicated W-axis motor, then inserted by the insertion shaft. The 2024 brochure states the machine supports direct jumper-wire insertion without tapes, and that a dual-feeder arrangement handles two wire specifications — 0.5 mm and 0.6 mm — at the same time. Southern Machinery documents this…
From a taped reel to a clinched lead in six stages
The sequence below is the machine's own description of its mechanism, taken from the S4000 series manual. Each stage names the subassembly that performs it, because when a line stops you need to know which of them to look at.
- The seven axes, in the machine's own names. Verified material Axis names and functions: S4000 Series Manual V1.1 section 2 and Software & Programming Manual V2.6.0.0 section 6.1.3. The manual notes that the absolute servo drive removes dozens of photoelectric switches, and that soft adjustment removes the need for mechanical adjustment of the span.
Where the documents disagree, both values stay on the page
The 2024 brochure and the series manual were written for different purposes and were not updated in step. Seven figures differ. Rather than average them or silently pick the friendlier one, Southern Machinery prints both and names the source, so you can put the right number in your own project file and ask us to confirm the rest at quotation stage.
What 20,000 points an hour actually buys you
The headline speed and the number you can plan a shift around are not the same number, and the S4000 documents are unusually honest about that: the brochure prints both. Here is how to use them without over-promising to your own production manager.
- 20,000 points per hour. This is the machine's stated ceiling — the axis speeds and cycle timings at their design limit, with an ideal component and an ideal board. It is the right number for a datasheet comparison and the wrong number for a capacity plan.
- 10,000 CPH actual. The 2024 brochure prints a separate actual-speed figure of half the ceiling. Use this one for shift planning and payback arithmetic. It is also the figure that survives contact with a real mix of parts, board transfer time and operator intervention.
- Your board's number. Neither figure tells you what your specific board will run at, because insertion count, part spread, span changes and board size all move the answer. That is what the free demo is for: ten of your bare boards, your component list, and a measured rate at the end of it.
- The throughput levers, ranked by how much they usually move the answer. Verified material To be confirmed Speed figures are quoted from the two source documents. The lever ranking is Southern Machinery's engineering judgement from the machine's mechanism description, not a measured throughput table — treat it as a discussion order for the demo, and confirm the real numbers on your own board.
Six decisions that shape the machine you receive
The S4000 is configured, not ordered off a shelf. These are the choices that change the price, the footprint and what the machine can run — and the ones worth settling before a purchase order rather than after.
- Feeder bank size. The feeder bank is modular, so the station count is specified at order and expanded later. Southern Machinery lists combinations from 5 to 60 stations; the manual lists 10, 20, 30 and 40 as configurable. Count the axial part numbers across the whole product family you expect to run in the next three years, then add two spare stations for the parts nobody has designed yet.
- Dual jumper-wire feeders. Two jumper-wire feeders let the machine run two wire specifications — 0.5 mm and 0.6 mm — without a changeover. The brochure states the machine supports direct jumper-wire insertion without tapes, and that it handles both reel-style and drum-style jumper wire packages with anti-jam feeding. If your boards use more than one wire gauge, this is the option that keeps both in the program at once.
- Automatic PCB loading. A standard automated PCB loading device is offered so the machine can sit in an in-line flow rather than being hand-fed. The brochure states this arrangement lets a single operator manage three to five machines. Conveying direction is selectable left-to-right or right-to-left, and a custom manual version is available if you want to start without the loader.
- Built-in air storage tank. The brochure lists a built-in air storage tank as a standard feature, described as smoothing the air supply so insertion quality stays consistent and maintenance effort drops. It matters most where the house air supply is shared with other machines and the pressure dips when a neighbour cycles.
- Built-in 3 kVA regulator. A built-in 3 kVA regulator is listed as standard, described as reducing circuit failures and downtime by holding the supply steady. The manual adds that the control system requires all electrical systems of the machine to be reliably grounded, and that the protection set includes an isolation transformer.
- Component height and board size. Standard component height allowance is 15 mm and the manual notes it is customisable on request. Maximum board size is listed as 330 x 300 mm in the manual and 400 x 300 mm in the brochure, and the manual adds that board size is customisable. If your panel is outside the standard envelope, say so at enquiry stage rather than at installation.
What commissioning actually involves
Most of the risk in an axial line sits in the two weeks around installation, not in the machine. The software manual documents the commissioning sequence in enough detail that you can see what your engineers will be asked to do.
- Axis zeroing and limits. Each axis is zeroed from the engineer page and the procedure differs per axis: the X axis moves to the far right and releases the coupling, the Y axis moves to the topmost position, the H axis needs the timing belt removed, the U axis the timing belt, the R axis the timing pulley, and the C axis the reducer coupling. Soft limits are then set from a displacement operation. This is also the…
- Program creation on the machine. A new program starts by marking the insertion positions on the board at 0 degrees and then at 90 degrees, positioning the board on the middle rail, and stepping the camera to each hole to confirm coordinates. The program list stores insertion sequence, coordinates, rotation angle R with sign for direction, span, feeder number, component model and a program function code where OS is an offset…
- Panelisation for multi-board panels. Where several small boards share one panel, the software builds the program from one board. You complete the first board's program, enter the panel count in X and Y, acquire the top-left and bottom-right coordinates, calculate spacing, preview the result, choose the sorting method and execute. Automatic coordinate correction then re-checks every generated position.
- Diagnostics and feeder testing. The equipment status page shows the live state of every input and output signal, so a stuck cylinder or a blocked photoelectric sensor is visible as a state change rather than a guess. Each station can be driven individually from the feeder test page, one operation per click. Production information is counted automatically and saved into a record folder.
What happens after the machine lands
Southern Machinery has been selling and supporting auto insertion equipment since 2011, and has shipped more than fifty automatic insertion machines into Brazil, India, Malaysia, Indonesia, Thailand, Turkey, Saudi Arabia, Ecuador, Colombia and Argentina. The support model is the same one that kept those machines running.
Videos
Clips aus dem YouTube-Kanal von Southern Machinery. Von YouTube wird erst etwas geladen, wenn Sie auf Abspielen drücken.
Kataloge und Dokumente
- PDFS4000 Axial Insertion machine 2024 — product brochureS4000 machine documents
- PDFS4000 Axial Insertion Machine — product descriptionS4000 machine documents
- PDFAxial Inserter S4000 — overview sheetS4000 machine documents
- PDFS-4000H Jumper Wire Axial InserterS4000 machine documents
- DOCS4000 Axial Insertion Machine — users manualS4000 machine documents
- 3DS4000H jumper-wire axial inserter with PCB loader3D drawings and line layouts
- 3DS4020A axial insertion machine, 3D view3D drawings and line layouts
- 3DSMT axial taped feeder, 3D view3D drawings and line layouts
- 3DTHT axial and radial PCBA line layout3D drawings and line layouts
- XLSXTHT insertion ROI calculatorWorksheets and checklists
- XLSXTHT auto insertion ROI worksheetWorksheets and checklists
- PDFAuto insertion readiness checklistWorksheets and checklists
- PDFPCB assembly requirements for auto insertionWorksheets and checklists
- LIBBrowse the full Southern Machinery resource libraryWorksheets and checklists
- 3DProduct catalogue board
- 3DYouTube video catalogue
Technische Notizen
ARTICLE 01The Cheapest Axial Quotation Is Not the Cheapest Board
Three suppliers quote the same axial inserter. The lowest number wins the order, and eighteen months later nobody can explain why the through-hole department still costs what it did. Full articles are in English. The summary above carries the argument in your language. Start with the moment the comparison actually…
ARTICLE 02Twenty Thousand Points an Hour Is a Specification, Not a Forecast
The number on the datasheet decides whether you get the budget. The number on the shift report decides whether you keep your credibility. Full articles are in English. The summary above carries the argument in your language. Every insertion machine is sold on a maximum rate, and every production manager has been…
ARTICLE 03A Sixty-Station Machine You Buy Once and Configure Five Times
Most axial machines are specified against the job that justified them, and then asked to run a product family that did not exist when the order was placed. Full articles are in English. The summary above carries the argument in your language. Here is how the specification meeting usually goes. The engineering team…
ARTICLE 04Jumper Wire Is the Part That Stops Axial Lines
The machine handles diodes and resistors all day. Then it meets a jumper wire, and the shift stops being about throughput. Full articles are in English. The summary above carries the argument in your language. Ask anyone who has run an axial inserter what the worst part on the board is, and you will get the same…
ARTICLE 05Any Angle Is a Layout Decision, Not a Feature
Insertion at any angle is usually sold as a machine capability. It is more usefully understood as permission for your designer to stop routing around the machine. Full articles are in English. The summary above carries the argument in your language. Look at a through-hole layout drawn by someone who has spent years…
ARTICLE 06What Happens Between the Chain and the Board
An axial insertion happens in about a third of a second. Engineers who cannot name the stages inside that third of a second cannot diagnose a fault in it. Full articles are in English. The summary above carries the argument in your language. The scene is familiar. The machine is bending leads wrong, or cutting…
Vollständige Artikel auf der interaktiven Produktseite lesen →
Häufige Fragen
Wie hoch ist die reale Bestückgeschwindigkeit des S4000?
Es sind zwei Werte veröffentlicht, die sich um den Faktor zwei unterscheiden. Die Produktbroschüre von 2024 nennt eine Höchstgeschwindigkeit von 20.000 CPH und eine reale Geschwindigkeit von 10.000 CPH. Das Serienhandbuch nennt 20.000 Punkte pro Stunde als Maximum. Betrachten Sie den ersten Wert als Spezifikationsgrenze und den zweiten als Planungszahl, und bestätigen Sie die Rate Ihrer eigenen Platine in einem Vorführlauf, statt einen der beiden zu übernehmen.
Welche Bauteile kann er bestücken?
Gegurtete Axialbauteile: Dioden, Widerstände und Drahtbrücken mit Anschlussdurchmessern von 0,3 mm bis 0,8 mm. Drahtbrücken aus der Trommel werden unabhängig über einen eigenen Mechanismus zugeführt. Die zulässige Bauteilhöhe beträgt standardmäßig 15 mm und kann auf Anfrage angepasst werden.
Kann er in anderen Winkeln als 0 und 90 Grad bestücken?
Ja. Die Platine liegt auf einem servoangetriebenen Drehtisch, und der Drehwinkel ist ein Feld im Bestückprogramm für jede Zeile, wobei das Vorzeichen Uhrzeigersinn oder Gegenuhrzeigersinn angibt. Dadurch kann ein Layout diagonale Bauteile verwenden, ohne Drahtbrücken hinzuzufügen, um die Einschränkung zu umgehen.
Wie viele Feederstationen brauche ich?
Die Broschüre nennt Konfigurationen mit 5, 10, 20, 30, 40, 50 und 60 Stationen; das Handbuch nennt 10, 20, 30 und 40 als bedarfsgerecht konfigurierbar. Zählen Sie die verschiedenen axialen Teilenummern über Ihre ganze Produktfamilie – nicht nur die aktuelle Platine – und planen Sie Reserve ein. Die Bank ist modular und lässt sich später erweitern.
Was passiert bei zwei verschiedenen Drahtbrückenstärken?
Die Maschine wird mit doppelten Drahtbrücken-Feedern angeboten, die zwei Drahtspezifikationen wie 0,5 mm und 0,6 mm ohne Umrüstung verarbeiten; die Zuführung deckt sowohl Rollen- als auch Trommelgebinde mit staufreier Zuführung ab. Verwenden Ihre Platinen mehr als eine Stärke, wählen Sie diese Option.
Ist er bereit für MES und Industrie 4.0?
Die Steuerungsplattform läuft unter Windows auf einem Industrie-PC mit busbasierter Bewegungssteuerkarte, und die Software schreibt Produktionsdaten in einen MES-kompatiblen Ordner. 4G-IoT und Black-Box-Datenaufzeichnung sind als verfügbar aufgeführt. Produktionsinformationen werden automatisch gezählt und in einem Protokollordner gespeichert, mit Speicher- und Löschfunktion auf der Statistikseite.
Kann ein Bediener mehr als eine Maschine betreuen?
Ja, mit der Option für automatische Platinenzuführung. Die Broschüre gibt an, dass eine standardmäßige automatische Platinenzuführung es einem einzelnen Bediener ermöglicht, drei bis fünf Maschinen zu betreuen, und dass sich die Maschine in bestehende Produktionslinien integriert. Die Förderrichtung ist links-nach-rechts oder rechts-nach-links wählbar, und eine kundenspezifische Version mit manueller Beladung ist erhältlich.
Was beinhaltet die kostenlose Vorführung?
Southern Machinery bietet eine kostenlose Vorführproduktion mit zehn unbestückten Platinen, die Sie liefern, einen Live-Stream der laufenden Maschine, damit Sie in Echtzeit zusehen können, und anschließend einen schriftlichen Bewertungsbericht. Senden Sie die Platinen, die Liste der Axialbauteile und das Monatsvolumen; der Bericht kommt mit dem gemessenen Ergebnis zurück.
Warum haben manche Werte auf dieser Seite zwei Angaben?
Weil die Broschüre von 2024 und das Serienhandbuch für unterschiedliche Zwecke geschrieben und nicht gleichzeitig aktualisiert wurden. Sieben Werte unterscheiden sich – Maschinenabmessungen, Gewicht, maximale Platinengröße, Rastermaß, Anzahl der Feederstationen, Luftdruck und die Geschwindigkeitsangabe. Statt sie zu mitteln oder einen auszuwählen, zeigt die Seite beide mit Quelle, damit Sie Stellplatz und Luftversorgung richtig auslegen und den Rest beim Angebot mit uns bestätigen können.
Wie groß ist die Stellfläche, und passt sie in meine Halle?
Die Broschüre nennt 1700 x 1500 x 1600 mm und 880 kg. Das Handbuch nennt eine Hauptmaschine von 1780 x 1500 x 1600 mm plus eine Hilfsmaschine von 500 x 900 x 1000 mm sowie separate Materialstationsgestelle von 850 x 900 x 1360 mm für zehn Stationen und 1400 x 900 x 1360 mm für zwanzig. Die Konfiguration entscheidet; senden Sie uns die Maße Ihres Stellplatzes, und wir planen die Aufstellung.
Wie lange dauert die Installation, und wer führt sie durch?
Installation und Inbetriebnahme sind enthalten und werden von Ingenieuren von Southern Machinery durchgeführt, gefolgt von Bediener- und Wartungsschulung. Das Softwarehandbuch dokumentiert das Nullen der Achsen und den Ablauf der Programmerstellung im Detail, sodass Ihr Team Programme und Nutzenpläne vorbereiten kann, während die Maschine unterwegs ist.
Was sollte ich mit einer Anfrage senden?
Drei Dinge: die Liste der Axialbauteile mit Anschlussdurchmessern und Rastermaßen, Abmessungen und Dicke der Platine sowie das monatliche Platinenvolumen. Haben Sie eine Platinenzeichnung, senden Sie diese ebenfalls. Mit diesen drei Angaben können wir Ihnen die Größe der Feederbank nennen, sagen, ob ein Teil eine Sonderanfertigung braucht, und wie die Bestückzeit aussehen wird.
Ähnliche Produkte

THT-Bestück- und Wellenlötlinie für Handy-Ladegeräte – smarte EMS-Leiterplattenbestückung
Schlüsselfertige THT-Linie für Leiterplatten von Handy-Ladegeräten und Netzteilen: Platinenlader, Radialbestücker S3010A, Terminal- und Odd-Form-Bestücker S7020, Vier-Kopf-Odd-Form-Zelle mit Wendel- und Schüttgutfeedern, Wellenlötanlage S-WS350 und Auslauf. Interaktive 3D-Linie, Spezifikationen mit Quellen, Videos, Kataloge und Amortisationsrechnung.
Radialbestückautomat S3000 für die smarte EMS-THT-Leiterplattenbestückung
Radialbestückautomat S3000 für die THT-Leiterplattenbestückung: gegurtete Radialbauteile mit bis zu 20.000 CPH, Bestückwinkel 0–360 Grad, 10 Feederstationen und Lochkorrektur per Bildverarbeitung.
S7900 Odd-Form-Bestückautomat – Lösung für die smarte EMS-THT-Leiterplattenbestückung
Odd-Form-Bestückautomat S7900: 2, 4 oder 6 Servoköpfe, 0,6–0,8 s pro Bauteil, Platinendicke 0,6–2,0 mm, Bestückung 0–360 Grad, vier Umbiegemuster und Wendel-, Gurt-, Stangen- und Trayfeeder auf einer Plattform. Mit Aufteilung einer 36-zeiligen THT-Stückliste und einer Offenlegungstabelle aus drei Dokumenten.

S-300B Radial-Biege- und Gurtmaschine
Radial-Biege- und Gurtmaschine S-300B: formt das Anschlussraster, prüft Polarität und Wert und gurtet dann 180 ± 20 Bauteile pro Minute, in Box oder auf Rolle.
Einige technische Angaben auf dieser Seite (Tabellen, Dokumenttitel) erscheinen wie veröffentlicht auf Englisch.
Angebot anfordern: Axialbestückautomat S4000 für die smarte EMS-THT-Leiterplattenbestückung
Senden Sie Ihre Platine, Bauteilliste oder Ihr Maschinenmodell, und wir antworten mit einer Konfiguration und einem Angebot. Preise werden projektbezogen kalkuliert.